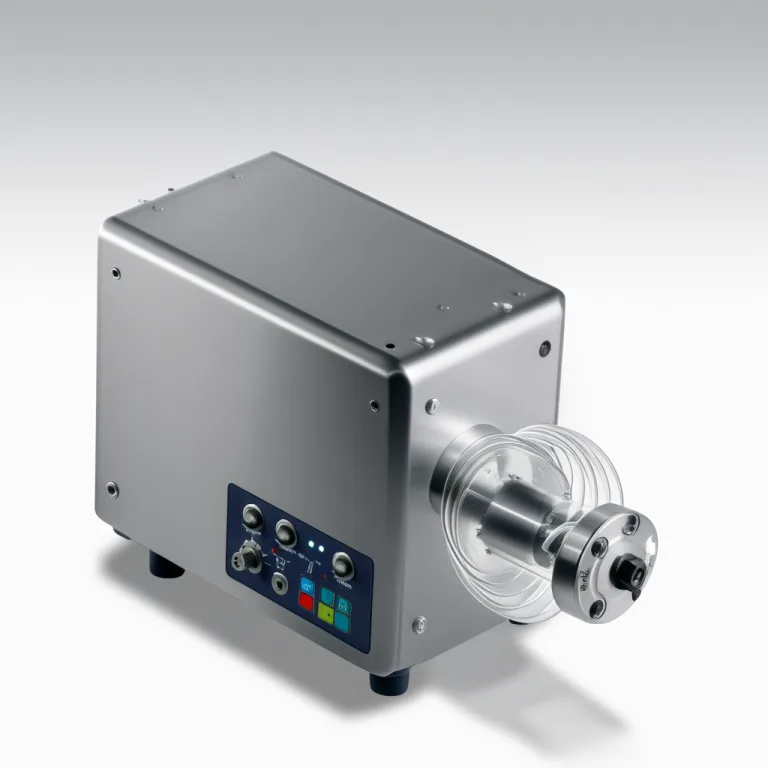
Peristaltic Chemical Pump
Peristaltic Chemical Pump for industrial applications.
About Peristaltic Chemical Pump
Peristaltic Chemical Pump for industrial applications.
| Domain | chemical |
|---|---|
| Product Family | Pumps |
Who Works With Peristaltic Chemical Pump?
7 engineering roles are connected to Peristaltic Chemical Pump based on verified research evidence.
Maintenance Technician
Field Service Technician
Field Service Technician is a widely recognized professional role in industrial automation, specifically tasked with on-site deployment, commissioning, diagnostics, preventive/predictive maintenance, and repair of motor drives including VFDs. The role is standardized across OEMs (e.g., ABB, Danfoss, Siemens) and aligns directly with the product context of variable frequency drives used for motor speed/torque control. While specialization in drives may exist, 'Field Service Technician' itself is not product-specific — it's a canonical, cross-domain role.
Process Engineer
Beverage Process Engineer is a recognized engineering role specializing in process design, validation, and compliance for beverage manufacturing systems. While 'Beverage' denotes industry context (not product-specific specialization), the role directly engages with ribbon blenders — particularly in specification, commissioning (including IQ/OQ), CIP/SIP integration, and 3-A sanitary validation — all cited in job listings. 'Process Engineer' is the canonical, general professional title; 'Beverage' reflects domain application, not an inseparable part of the core role definition.
Applications Engineer
Applications Engineer is a well-established professional role in industrial equipment sectors, especially for process machinery like ribbon blenders. In the beverage context, they bridge technical capability and customer process requirements — advising on blender selection, configuration (e.g., material of construction, drive type, explosion protection), integration into production lines, and operator training. The evidence explicitly links them to ribbon blender support (installation, FAT/SAT, training), confirming functional relevance.
Chemical Operator
Chemical Operator is a widely recognized, standardized occupational title in industrial chemical processing environments. It denotes a frontline operations role responsible for monitoring, controlling, and responding to process equipment—including pumps like peristaltic chemical pumps—during production. The role is not product-specific (i.e., not 'Peristaltic Pump Operator'), but inherently interacts with such equipment in its operational context. Evidence from job boards (Indeed) confirms its use alongside Maintenance Technician and Process Engineer in pump-relevant hiring contexts.
Design Engineer
Pump Operator
Peristaltic Pump Operator is a functional job title used in chemical process industries to denote personnel responsible for operating, monitoring, and performing basic interventions on peristaltic pumps in chemical feed systems. While 'Peristaltic' specifies the pump type, the core professional role is 'Pump Operator' — a widely recognized operations role in industrial chemical, water treatment, and pharmaceutical settings. Evidence confirms operator-level positions requiring hands-on experience with peristaltic metering pumps in chemical feed systems, supporting its legitimacy as a real-world operational role.